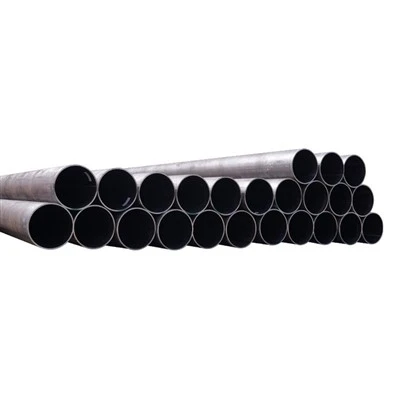
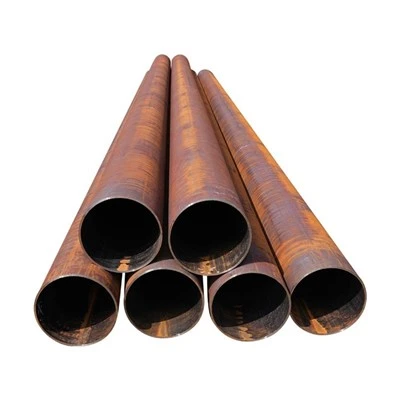
The chemical industry is characterized by its demanding operational environments, involving the transportation and containment of corrosive, high-temperature, and high-pressure fluids and gases. The integrity of piping systems and pressure vessels in this sector is paramount, as any failure can lead to severe safety hazards, environmental contamination, and significant economic losses. Longitudinal Submerged Arc Welded (LSAW) steel pipes, with their superior strength, precise manufacturing, and adaptability to specialized linings, have become a critical component in chemical processing plants and the fabrication of pressure vessels. Hebei Huayang Steel Pipe Co., Ltd., a leading manufacturer of high-quality LSAW steel pipes, explores their essential role in ensuring the safety and operational integrity within the chemical industry.
The Stringent Requirements of the Chemical Industry
Chemical processing and pressure containment applications impose rigorous demands on piping materials:
- Corrosion Resistance: Exposure to a wide range of aggressive chemicals (acids, alkalis, solvents) necessitates materials that can resist chemical degradation and maintain structural integrity.
- High-Temperature and High-Pressure Service: Many chemical reactions and processes occur at elevated temperatures and pressures, requiring pipes and vessels capable of safely containing these conditions.
- Material Purity and Non-Contamination: For certain chemical processes, preventing contamination of the transported media is crucial, demanding smooth internal surfaces and inert linings.
- Mechanical Strength and Toughness: Pipes and vessels must withstand operational stresses, thermal cycling, and potential external impacts without deformation or failure.
- Leak-Tightness: Absolute leak-tightness is critical to prevent the escape of hazardous substances, ensuring personnel safety and environmental protection.
LSAW steel pipes, especially when combined with appropriate material grades and protective linings, are uniquely suited to meet these stringent requirements, providing reliable and safe solutions for the chemical industry.
Advantages of LSAW Pipes in Chemical Applications
The inherent properties and manufacturing precision of LSAW steel pipes offer distinct advantages for chemical process pipelines and pressure vessel fabrication.
High Strength and Pressure Containment
LSAW pipes are manufactured from thick steel plates and feature a robust, full-penetration longitudinal weld seam. This construction provides exceptional mechanical strength, allowing them to safely contain high-pressure fluids and gases common in chemical processes. Their ability to be produced with significant wall thicknesses (up to 50mm) makes them ideal for heavy-duty applications, including high-pressure process lines and components of large pressure vessels.
Excellent Weld Integrity and Reliability
The dual internal and external submerged arc welding process, combined with rigorous non-destructive testing (NDT), ensures a high-quality, defect-free weld seam. This superior weld integrity is paramount in the chemical industry, where the failure of a weld could have catastrophic consequences. The reliability of LSAW welds contributes directly to the overall safety and operational uptime of chemical plants.
Adaptability to Corrosion-Resistant Linings
While standard carbon steel LSAW pipes provide structural strength, their internal surfaces can be protected with specialized corrosion-resistant linings to handle aggressive chemical media. These linings, such as various types of epoxy, rubber, or even glass, create an inert barrier between the steel and the chemical, preventing corrosion and ensuring the purity of the transported substance. The smooth internal surface of LSAW pipes provides an excellent substrate for these linings.
Large Diameter and Customization
LSAW pipes can be produced in large diameters (up to 1422mm or 56 inches), which is beneficial for high-volume chemical transfer lines or for fabricating large-capacity pressure vessels and storage tanks. The ability to customize pipe lengths, diameters, and material grades (including specialized alloys for specific chemical resistance) allows for tailored solutions that precisely fit the unique demands of complex chemical processes.
Structural Stability for Pressure Vessels
In the fabrication of pressure vessels, LSAW pipes can serve as the main cylindrical body or as components for larger vessels. Their consistent dimensions, high strength, and reliable welds contribute to the overall structural stability and safety of these critical containment units, which are designed to operate under significant internal pressures.


Diverse Applications in the Chemical Industry
LSAW steel pipes are integral to a wide array of chemical industry applications:
- Process Pipelines: Used for transporting various chemicals, acids, alkalis, and solvents within chemical plants, often under high pressure and temperature conditions.
- Storage Tanks and Reactors: Form the structural components for large-scale storage tanks and chemical reactors, providing robust containment for hazardous or valuable substances.
- Heat Exchanger Components: Employed in the construction of heat exchangers where robust, corrosion-resistant piping is required to manage temperature transfers in chemical processes.
- Pressure Vessels: Utilized as the main body or components in the fabrication of pressure vessels, such as distillation columns, scrubbers, and separators, designed to operate under specific pressure regimes.
- Effluent Treatment Lines: Transporting industrial wastewater and chemical effluents to treatment facilities, often requiring corrosion-resistant linings.
Hebei Huayang: Your Partner for Chemical Industry Solutions
Hebei Huayang Steel Pipe Co., Ltd. is a trusted provider of LSAW steel pipes specifically engineered for the rigorous demands of the chemical industry and pressure vessel fabrication. Our pipes are manufactured to the highest international standards, including API 5L, ASTM A671/A672, and EN standards, ensuring their suitability for critical chemical applications. With production capabilities for LSAW pipes up to 1422mm in diameter and 50mm in wall thickness, we offer robust solutions for even the most challenging chemical projects.
We provide customized material grades (from Q235B to X80 and specialized alloys) and can facilitate the application of various internal corrosion-resistant linings and external anti-corrosion coatings to meet the precise requirements of your chemical process or pressure vessel. Partner with Hebei Huayang to ensure the safety, reliability, and longevity of your chemical infrastructure.
Key Specifications for LSAW Steel Pipes in Chemical Industry & Pressure Vessels at Hebei Huayang
|
Specification Category |
Details |
|
Outer Diameter (OD) |
406mm (16") – 1422mm (56") |
|
Wall Thickness (WT) |
7mm – 50mm |
|
Material Grades |
Q235B - X80 (Customizable, including specialized alloys) |
|
International Standards |
API 5L PSL1/PSL2, ASTM A671/A672, EN10217, EN10219 |
|
Internal Linings |
Epoxy, Rubber, Glass (customizable for chemical resistance) |
|
External Coatings |
3LPE, FBE (customizable for environmental protection) |
|
Key Applications |
Process pipelines, storage tanks, reactors, pressure vessels, effluent lines |
In conclusion, LSAW steel pipes are an indispensable component in the chemical industry and pressure vessel fabrication, providing the strength, integrity, and adaptability required for safe and efficient operations. By choosing Hebei Huayang Steel Pipe Co., Ltd., you are partnering with a manufacturer dedicated to delivering high-quality LSAW pipes that ensure the reliability and longevity of your critical chemical infrastructure. Contact us today to discuss your project needs and explore our comprehensive range of LSAW pipe solutions.